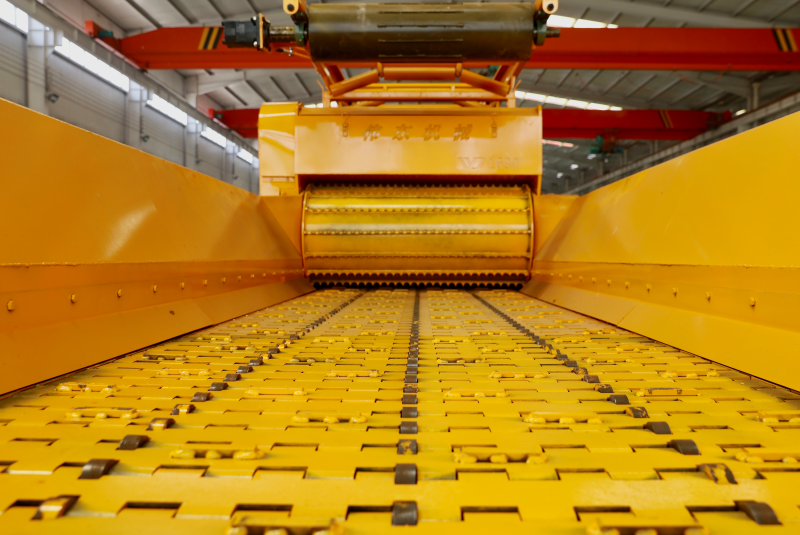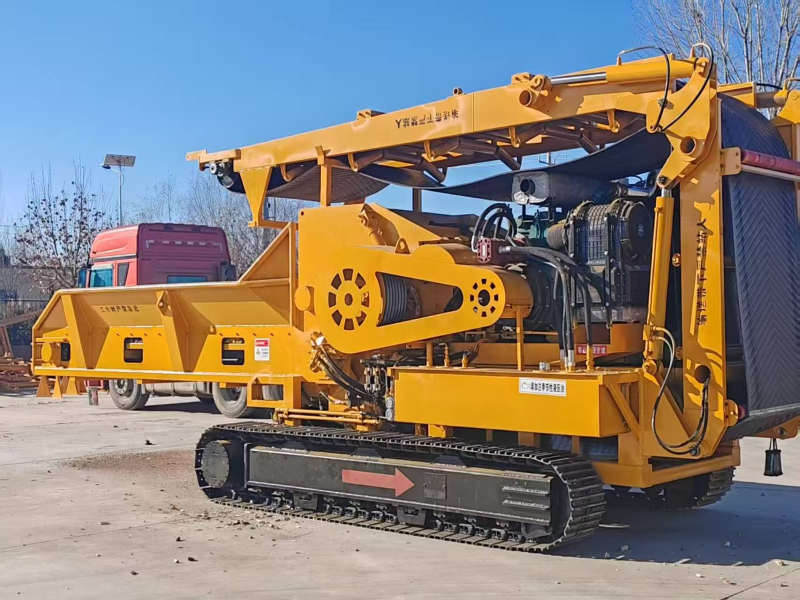
Inspection intervals for a horizontal grinder processing logging slash should reflect the machine manual, actual material and events observed on site. A clock alone cannot tell an operator whether tangled branches have damaged a feed component or whether a wet, soil-bearing load has accelerated wear. This field worksheet separates checks before operation, observations during production, planned service and event-triggered inspections. It does not prescribe a universal number of operating hours. Record findings against the machine identification, configuration and operating conditions so the next shift can act on them.
Build the inspection schedule from the exact machine
Begin with the manufacturer’s operating and maintenance manuals for the installed grinder, engine or drive, hydraulic system and optional equipment. List each required inspection, the method, the person qualified to perform it and the required isolation state. The model’s service schedule takes priority over a generic article or another plant’s practice. Add local legal requirements and site procedures where applicable. Give every item a record field for date, meter reading if available, finding, corrective action and return-to-service signoff. An interval is useful only if the assigned crew can perform the check safely and retain its result.
Record the material that changes inspection needs
Logging slash can contain long forked limbs, foliage, bark, soil-bearing roots and material from several landings. Document which lots are fresh, wet, muddy or likely to contain foreign objects. Note the feed preparation and loader method. These observations help a supervisor decide when an additional condition check is warranted under the manufacturer’s guidance. A logging slash feed-characteristics guide can help standardize the incoming description. Do not claim that a particular species or moisture level automatically requires a fixed shorter interval without evidence from the machine and its operating history.
Complete the pre-start walkaround
Before operation, follow the model’s approved pre-start sequence. Check visible guards, access doors, emergency stops, warning devices, leaks, loose hardware, feed and discharge paths, and the condition of wear components that can be viewed safely. Confirm that scheduled service and unresolved defects have been reviewed. Record any damage or missing protection and keep the equipment out of service until the responsible person clears it. Test safety functions only as the manufacturer and site procedure direct. The safe-feeding checklist for slash explains why this walkaround belongs before the loader starts moving material.
Watch trends during a controlled run
Operators should monitor the indications provided on the actual machine, along with feed behavior, vibration, abnormal noise, hydraulic response and discharge flow. Compare a suspect observation with the baseline for the same material and configuration. A sudden change after a contaminated load deserves attention even if the planned service point is far away. Record when the symptom began, the material lot and the action taken. Do not diagnose a bearing, rotor or drive fault from sound alone. Stop under the machine’s instructions when a warning, unusual condition or unsafe feed appears, and ask qualified personnel to inspect it.
Inspect after a foreign-object or blockage event
Wire, metal, stone and other objects can be hidden inside a slash pile. If an object is suspected or a jam occurs, stop feeding and apply the model-specific shutdown, energy-isolation and clearing procedure. Only trained people should approach the affected area. Inspect the relevant feed, cutting, screen and discharge components after the machine is made safe, using the manufacturer’s criteria. Note the object, source lot, damage found and part disposition. A restart without inspection can turn a small issue into a larger interruption. The whole-tree contamination control note offers a related source-sorting method, but tangled slash merits its own event log.
Review wear parts and fasteners with evidence
Use the manufacturer’s wear limits, torque instructions and replacement procedure for teeth, hammers, cutters, screens, belts and other fitted parts. Photograph or measure condition consistently where the manual permits. Compare remaining serviceability with accepted output and material handled, rather than copying an advertised life figure from a different feedstock. Record any change in product size or increased regrind that might call for inspection. The wear cost per accepted ton worksheet shows how parts, downtime and rejected product enter a purchasing comparison. Replace components as specified; do not run damaged parts solely to improve a cost estimate.
Keep the service window separate from operation
Plan inspections and replacement work around qualified staff, isolation, lifting equipment, spare parts and access to the machine. A planned service window is more than the minutes needed to fit a part. Include cooling, cleaning, access opening, inspection, fitting, checks and authorized restart in the work order. If a mobile crew serves multiple landings, list which parts and tools travel with it and which require a service vehicle. Coordinate this with the production plan so operators do not feel pressured to defer a required check. The actual intervals and tasks must remain those approved for the exact configuration.
Use a defect decision table
For each finding, record whether the equipment can continue under the manual, needs monitored operation under an approved instruction, or must stop pending repair. Define who can make that decision. Do not leave an ambiguous note such as “watch it” without the component, limit, next check and owner. Keep temporary controls visible to the next shift, and close them only after the required verification. If several similar faults recur, review feed contamination, loading practice, site conditions and service method together. A recurring issue may be caused upstream rather than by one isolated component.
Measure whether the interval plan works
Review completed checks against unplanned stops, repair findings, parts use and accepted output. Separate machine operating hours from total shift hours and note material changes. If events repeatedly occur between scheduled checks, consult the manufacturer about a condition-based adjustment. If frequent checks reveal no change, do not remove them without reviewing the manual and the site’s risk assessment. Record who approved any revision and when it takes effect. This creates a traceable maintenance plan rather than a copied checklist.
Prepare a supplier discussion
Send the supplier the model and configuration, manual revision, slash description, event log, component photographs, service history and output requirements. Ask which inspection tasks are mandatory, which can vary with material and what evidence should trigger additional checks. The horizontal grinder product range gives equipment context. A horizontal wood grinder overview can help a buyer understand the category, while the engineering contact page is the place to resolve model-specific inspection questions. Confirm the resulting schedule in the project documentation before relying on it for staffing or budget.